

Steel Structure Technical Specifications
This page sets out the technical basis for steel structures fabricated by Truong Thinh Corp: steel grades and welding scope, bolting, surface preparation and coating, the inspection plan, and the design codes buyers commonly specify. Values are general references; the project specification and the engineer of record decide the final values for each building.
How to Read These Specifications
- Company scope items come from Truong Thinh Corp certificates and processes, for example the welding scope of EN ISO 3834-2:2021.
- General reference items come from widely used standards and typical industry ranges. They help you prepare a brief and compare quotations. They are not a guarantee for a specific building.
- Where your project specification differs, the project specification governs and the quotation states the agreed value.
Structural Steel Grades
| Grade | Standard | Minimum yield strength | Note |
|---|---|---|---|
| S235JR | EN 10025-2 | 235 MPa (thickness up to 16 mm) | General plates and sections |
| S275JR | EN 10025-2 | 275 MPa (thickness up to 16 mm) | Common for secondary members |
| S355JR / S355J2 | EN 10025-2 | 355 MPa (thickness up to 16 mm) | Common for primary frames; J2 adds impact toughness |
| A36 | ASTM A36 | 250 MPa (36 ksi) | Plates and shapes |
| A572 Grade 50 | ASTM A572 | 345 MPa (50 ksi) | Higher-strength plates and shapes |
| SS400 | JIS G3101 | 245 MPa (thickness up to 16 mm) | Common in JIS-based projects |
| Q235B / Q355B | GB/T 700 / GB/T 1591 | 235 / 355 MPa (thickness up to 16 mm) | Equivalent to S235 and S355 ranges |
Company scope: the welding certificate covers parent material groups 1.1 and 1.2 of ISO/TR 15608, that is carbon-manganese steels with a specified minimum yield strength up to 360 MPa. Grades above that range are outside the certified welding scope and are confirmed before an order is accepted. Minimum yield strength falls as thickness increases for the EN, JIS and GB grades; the standard gives the value for each thickness range. Every delivery of steel is traced by heat number against a mill test certificate to EN 10204 type 3.1.
Welding
| Item | Specification | Basis |
|---|---|---|
| Quality system | Comprehensive quality requirements for fusion welding | Company scope: EN ISO 3834-2:2021, certified by Bureau Veritas |
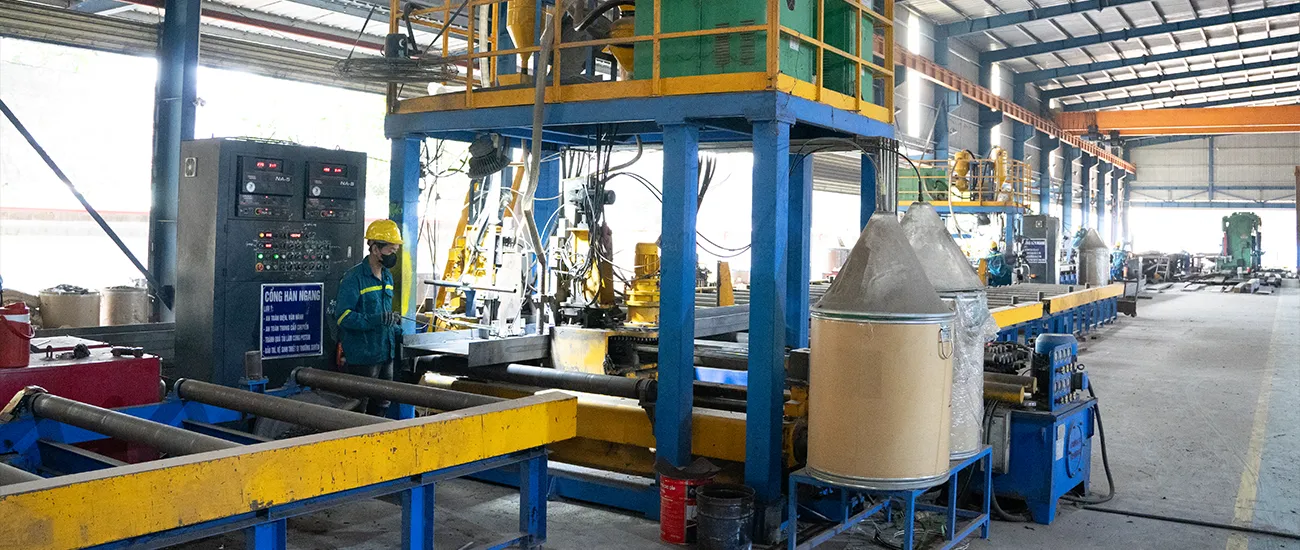
| Welding processes | Process 121 (submerged arc welding with one wire electrode) and process 136 (tubular cored metal arc welding with active gas shield) | Company scope: ISO 4063 processes on the certificate |
| Parent material groups | 1.1 and 1.2 | Company scope: ISO/TR 15608 groups on the certificate |
| Welding coordination | Welding coordinators appointed under ISO 14731 | Company scope: named on the certificate annex |
| Procedure qualification | Welding procedure specifications and qualification records to ISO 15614-1 or AWS D1.1 | General reference |
| Welder qualification | Welders qualified to ISO 9606-1 or AWS D1.1 | General reference |
| Weld quality level | ISO 5817 level C for statically loaded structures; level B where fatigue or the specification requires it | General reference |
| Inspection | Visual inspection of all welds; magnetic particle and ultrasonic testing to the extent in the project specification, by qualified personnel | General reference; ultrasonic testing level II staff are named in the certificate annex |
Bolting and Connections
| Item | Specification |
|---|---|
| Structural bolts | ISO 898-1 class 8.8 (minimum yield 640 MPa, tensile 800 MPa) and class 10.9 (minimum yield 940 MPa, tensile 1,040 MPa); or ASTM A325 for ASTM-based projects |
| Anchor bolts | ASTM F1554 grade 36 (250 MPa yield) or grade 55 (380 MPa yield), or the grade named in the foundation drawings |
| Tightening | Snug-tight or pretensioned, as the connection design requires; stated on the erection drawings |
| Connection design | Checked in the design model and shown on the shop drawings (Tekla Structures) |
| Base plates and splices | Dimensioned for the member forces and the anchor bolt layout in the foundation drawings |
Surface Preparation and Coating
Blast cleaning to Sa 2½ (ISO 8501-1) is the standard preparation before painting. The coating system and its thickness are set from the corrosivity category of the site (ISO 12944) and the design life you require. Dry film thickness is measured on the finished coating.
| Corrosivity category (ISO 12944) | Typical environment | Indicative total dry film thickness for medium durability |
|---|---|---|
| C2 low | Unheated buildings, rural areas | About 80 µm or more |
| C3 medium | Urban and industrial areas with moderate pollution, food plants | About 120–160 µm |
| C4 high | Industrial areas and coastal areas with moderate salinity, chemical plants | About 200–240 µm |
| C5 very high | Industrial areas with aggressive atmosphere, coastal areas with high salinity | About 280–320 µm |
Durability classes in ISO 12944 are low (2 to 7 years to first major maintenance), medium (7 to 15), high (15 to 25) and very high (over 25). Film thickness values above are indicative; the coating manufacturer data sheet and your specification decide the system.
Inspection and Test Plan
A typical plan for a project is shown below. The plan agreed in the order is the one that applies.
| Stage | Check | Record |
|---|---|---|
| 1. Material receiving | Heat number, grade and dimensions against the mill test certificate (EN 10204 type 3.1) and the order | Material traceability file |
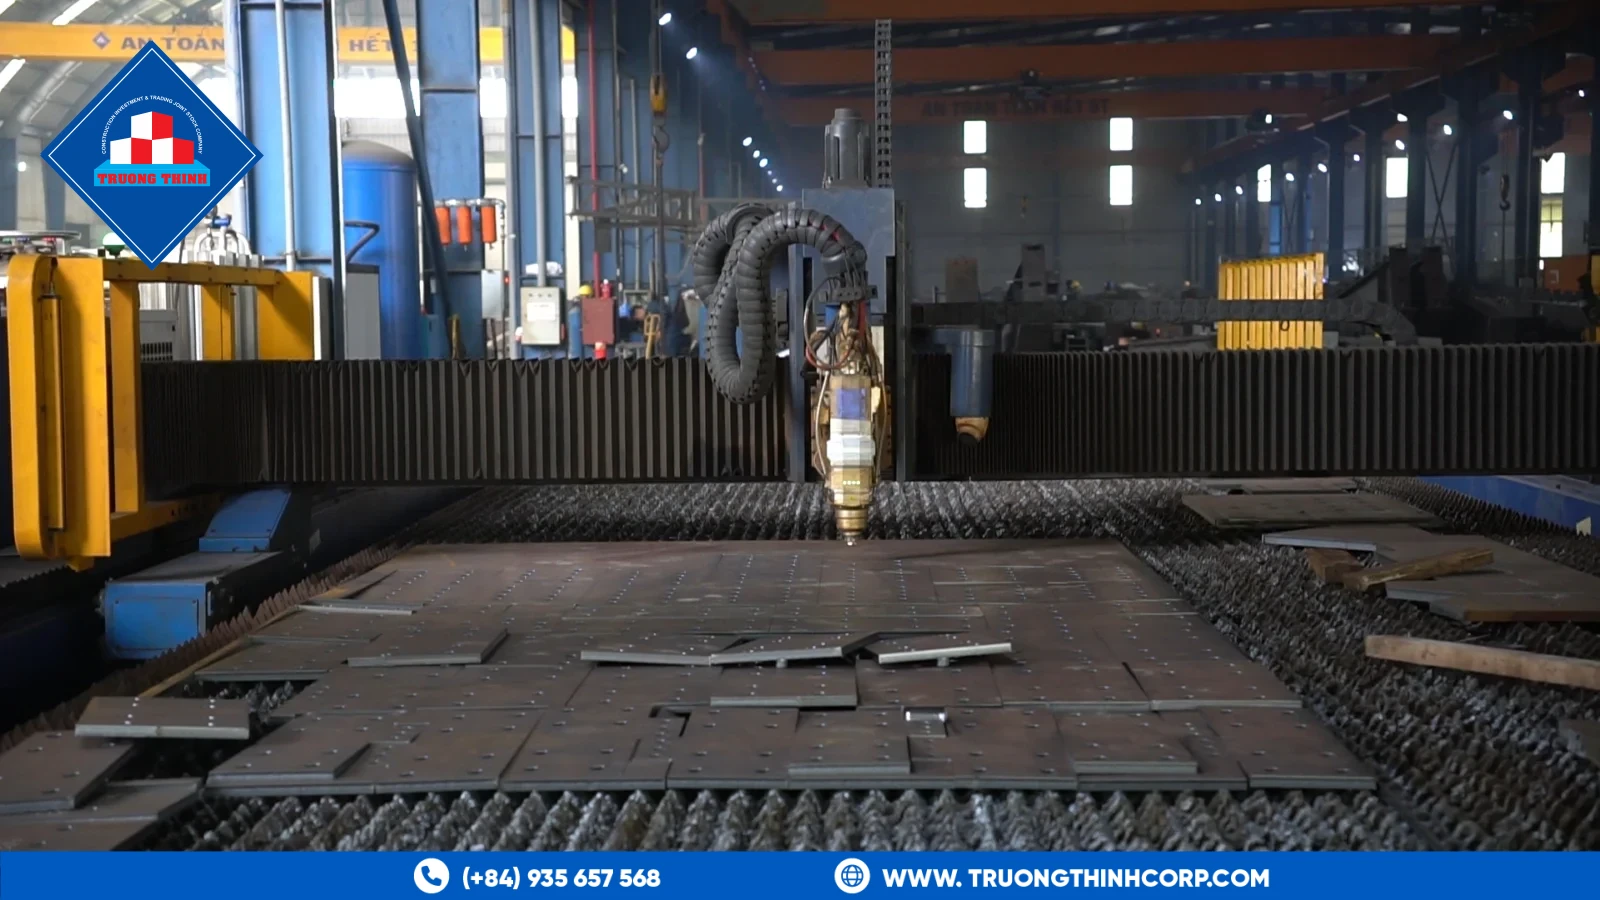
| 2. Cutting | Member dimensions and edge quality against the shop drawing | Cutting report |
| 3. Fit-up | Alignment, root gap and weld preparation before welding | Fit-up record |
| 4. Welding | Welding procedure, welder identity and visual inspection of all welds | Weld record |
| 5. Non-destructive testing | Magnetic particle and ultrasonic testing to the specified extent; acceptance to ISO 5817 | NDT report |
| 6. Dimensional check | Length, straightness, camber and bolt-hole positions against the drawings and the tolerance class in the specification | Dimensional report |
| 7. Blasting and coating | Sa 2½, surface profile, dry film thickness and adhesion when specified | Coating report |
| 8. Packing and marking | Member marks against the erection drawings and the packing list | Packing list |
Design Codes Commonly Specified by Market
The owner or the engineer of record names the governing codes. Truong Thinh Corp designs and details in SAP2000 and Tekla Structures to the codes your project states.
| Market | Steel design | Wind and seismic |
|---|---|---|
| Vietnam | TCVN 5575 | TCVN 2737 (loads and actions), TCVN 9386 (seismic) |
| Malaysia | MS EN 1993 (Eurocode 3) with the Malaysian national annex | MS 1553 (wind) |
| Singapore | SS EN 1993 (Eurocode 3) with the Singapore national annex | SS EN 1991-1-4 (wind) |
| Philippines | NSCP 2015, based on AISC 360 | NSCP 2015, based on ASCE 7 |
| Australia | AS 4100 | AS/NZS 1170.2 (wind), AS 1170.4 (earthquake) |
| Projects on US codes | AISC 360 | ASCE 7 |
Load values come from the governing code and the site data. They are not given as generic figures on this page.
Typical Ranges for Single-Storey Steel Buildings
These ranges describe what is common for pre-engineered and conventional single-storey buildings. The design for your site sets the actual values.
| Parameter | Typical range | Note |
|---|---|---|
| Clear span | About 20–60 m between columns of a frame | Longer spans use trusses or heavier built-up frames |
| Eave height | About 4–15 m | Higher for racking or process equipment; set by the layout |
| Bay spacing | Commonly 6–9 m, up to about 12 m | Wider bays suit heavy cladding or crane loads |
| Roof slope | Commonly about 1:10 (5.7°) | Set by the roof panel and the drainage design |
| Purlin and girt sections | Cold-formed C or Z sections, about 1.5–3.0 mm thick | Spacing commonly 1.2–1.8 m for purlins and 1.5–2.0 m for girts |
| Overhead cranes | Commonly up to about 20 t in a pre-engineered building | Heavier duty needs a design review and often a conventional frame |
Serviceability Limits Commonly Used
| Member | Typical vertical deflection limit | Note |
|---|---|---|
| Roof purlins and rafters | Span/180 to span/240 under live or wind load | Stricter when brittle finishes or ceilings are attached |
| Floor beams | Span/360 under live load | Stricter for sensitive equipment |
| Crane runway girders | Span/600 to span/1000, by crane duty class | CMAA 70 gives limits for each class |
The governing code and your specification decide the limits, and they also decide lateral drift limits, which depend on the cladding and the crane duty.
Documents Supplied with a Shipment
- Mill test certificates (EN 10204 type 3.1) for the steel
- Shop drawings and erection drawings, with member marks
- Welding procedure and welder qualification records, on request
- Inspection and test records for welding, dimensions and coating, as agreed in the order
- Packing list and, where a preferential tariff applies, the certificate of origin
What We Need from You to Fix the Final Values
- Governing design code and the loads, or the site data to derive them
- Span, eave height, bay spacing and crane details
- Environment of the site for the coating system, and the design life you require
- Any third-party inspection or documentation requirement
Request a quotation. Related: pre-engineered steel building manufacturer in Vietnam, steel structure for warehouse, industrial steel building, steel structure components, steel structure fabricator in Vietnam and the Company Facts page.
Frequently Asked Questions
What steel grades does Truong Thinh Corp fabricate?
Common carbon-manganese structural grades such as S235, S275, S355, A36, A572 Grade 50 and SS400. The welding certificate covers parent material groups 1.1 and 1.2 of ISO/TR 15608, up to 360 MPa minimum yield. Higher grades are confirmed before an order is accepted.
Which welding processes are certified?
The EN ISO 3834-2:2021 certificate from Bureau Veritas lists ISO 4063 process 121, submerged arc welding with one wire electrode, and process 136, tubular cored metal arc welding with active gas shield, for parent material groups 1.1 and 1.2.
What coating system is used?
The system depends on the corrosivity category of the site (ISO 12944) and the design life you require. Surfaces are blast cleaned to Sa 2½ before painting, and dry film thickness is measured on the finished coating. The quotation names the system and thickness.
Which design code does Truong Thinh Corp use?
The code your project states, for example TCVN, Eurocode, AISC or AS 4100. Design and detailing are done in SAP2000 and Tekla Structures. The owner or the engineer of record decides the governing code and the load values.
What documents come with the steel?
Mill test certificates to EN 10204 type 3.1, shop and erection drawings, inspection records as agreed in the order, a packing list and, on request, welding procedure and welder qualification records.
Are the typical ranges on this page guaranteed?
No. They are general references to help you prepare a brief. The project specification and the engineer of record set the final values for each building, and the quotation states the values agreed.
Free quotation · Reply within 24 working hours
Request a quotation for steel structure technical specifications
Tell us about your steel structure project. Our engineering and sales team will reply with a tailored proposal, usually within 24 working hours.
Need an answer faster? Call our engineers directly.
Mon–Fri 8:00–17:30 · Sat 8:00–12:00 (GMT+7)